OEM Introducer Sheath Essential Features to Evaluate Before Partnering with a Manufacturer
2026-09-26
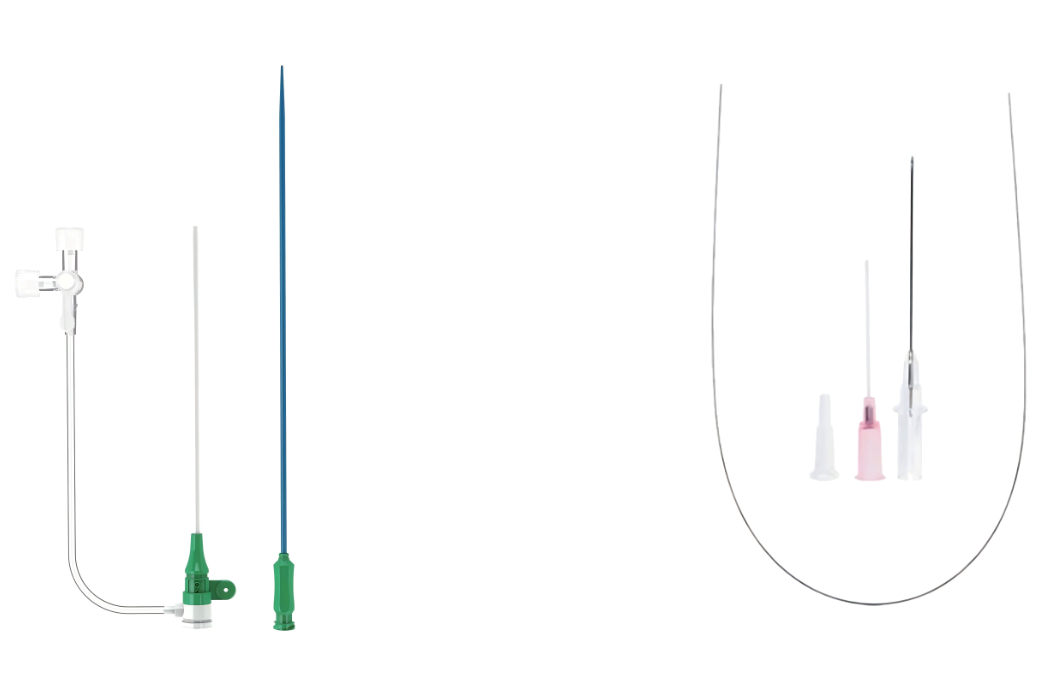
Every catheterization procedure depends on a deceptively simple component: the introducer sheath. When sourcing OEM sheaths, checking only price or lead time is a costly shortcut. At INT, we know that subtle differences in tip geometry, kink resistance, and hemostatic valve design determine whether a sheath performs reliably in the vessel or becomes a liability. Before you sign with a manufacturer, here are the features worth your toughest scrutiny.
Material Selection That Withstands Repeated Insertions
Choosing materials for repeated insertion starts with the contact alloy itself. Beryllium copper remains a top contender because it keeps its spring force after thousands of mating cycles, though the cost and heat treatment demands push some teams toward phosphor bronze. Bronze holds up reasonably well at room temperature, but it can relax faster in warm environments, so it is not always the safer bet. Selective plating makes a noticeable difference here: a nickel underlayer paired with a hard gold or palladium-nickel finish reduces micro-wear and keeps contact resistance stable far longer than bare copper alloys would.
The housing material is just as critical. High-temperature thermoplastics like LCP or PPA resist creep around retaining features, so the contacts stay put after repeated plugging and unplugging. Stainless steel shells or latches add useful stiffness when alignment is less than perfect during insertion. The right choice really depends on the expected cycle count. A design rated for a few hundred insertions can live with simpler material combinations, but anything rated for 10,000 cycles or more needs careful attention to oxidation, fretting, and gradual loss of normal force.
Coating Uniformity Across the Full Working Length
Coating weight that drifts by more than a few percent from lead edge to tail edge usually traces back to a handful of mechanical and rheological factors. Pump delivery can fluctuate as filters load or as the roll coating gap opens slightly with thermal expansion. Tension changes in the substrate, particularly on thin films or foils, also pull the wet film unevenly before it sets. Unless these variables are mapped over a full reel, operators often chase random defects instead of correcting the underlying drift.
One practical way to pin down the cause is to log coat weight at fixed intervals along the machine direction and compare that trend with pump speed, line speed, and die bolt settings. A gradual decline often points to viscosity shift from solvent evaporation or a slowly clogging feed line. A repeating wave usually correlates with roll eccentricity or a surging pump. Once the pattern is identified, small adjustments—like trimming the gap profile or raising the coating bath temperature—can bring the variation back within tolerance.
For longer runs, relying on manual samples is rarely enough. Closed-loop systems that feed a scanning gauge signal back to pump speed or die position help hold the profile flat without constant operator intervention. Still, it helps to separate machine-direction variation from cross-web variation before tuning the loop. Doing so prevents overcorrection and keeps the full working length within a tighter band than typical manual control allows.
Distal Tip Geometry and Guidewire Compatibility
The shape of a catheter's distal tip does more than ease insertion—it dictates how the device interacts with the vessel wall, branches, and lesions. A tapered, rounded profile lowers the risk of dissection while advancing through tortuous anatomy, whereas a more abrupt shoulder can create a ledge that catches on plaque or stent struts. In practice, the length of the taper matters just as much as its angle: a gradual transition gradually shifts radial force, letting the tip track over a guidewire without buckling or prolapsing into side branches.
Guidewire compatibility hinges on how the tip's inner lumen and distal aperture are finished. Too wide a clearance and contrast or saline leaks back around the wire; too tight and friction climbs, making wire exchanges feel sticky and unpredictable. Some designs use a short, stiffened segment just proximal to the tip to bridge the gap between a floppy wire and a stiffer shaft, while others rely on a stepped inner diameter that accepts wires from 0.014 to 0.038 inches without losing tactile feedback. The real test comes in tortuous vessels, where a tip that hangs up on a wire bend can double the force needed to cross a lesion.
A well-matched tip and wire combination often determines whether a case finishes in twenty minutes or becomes a salvage. Operators tend to pair a soft, shapable distal segment with a supportive wire for chronic total occlusions, while reserving stiffer, more columnar tips for straightforward anatomy where pushability trumps trackability. The geometry of the tip's transition zone—whether it necks down abruptly or blends over several millimeters—also affects how much torque reaches the distal end, a detail that often gets overlooked until a wire binds mid-rotation.
Sterilization Cycles That Preserve Polymer Integrity
Polymers respond to sterilization in ways that often surprise even seasoned engineers. The key isn't just reaching a target sterility assurance level—it's doing so without triggering chain scission, crosslinking, or plasticizer migration. Steam autoclaving, for instance, can hydrolyze susceptible backbones like polyesters or polyamides if moisture exposure lingers, while dry heat may accelerate oxidative degradation in polyolefins unless temperature ramps are tightly controlled. A cycle that preserves integrity typically pairs a moderate thermal load with rapid pressure equilibration, minimizing the time the polymer spends above its glass transition or heat deflection threshold.
Ethylene oxide and hydrogen peroxide gas plasma offer lower-temperature alternatives, yet each brings its own stress vector. EO can penetrate amorphous regions but leaves residues that may plasticize or craze certain engineering resins if aeration is too brief. Vaporized hydrogen peroxide, while residue-free on the surface, can embrittle polycarbonate or acrylics through radical attack at carbonate ester linkages. The most forgiving cycles often combine short exposure windows with aggressive post-sterilization vacuum pulls, stripping residual sterilant before it can diffuse deeper than a few microns. Material selection matters less than cycle tuning in many cases—small adjustments to dwell time, humidity setpoint, and chamber evacuation rate can extend a polymer's functional life by orders of magnitude.
Validation isn't just biological; it's rheological and mechanical. Post-cycle tensile modulus, impact strength, and molecular weight distribution tell you whether the sterilization left the polymer chain architecture intact. A well-designed cycle will show no statistically significant shift in melt flow index or glass transition temperature across three consecutive runs. For implantable or single-use devices, this means the polymer still performs as molded—no warpage from uneven thermal gradients, no microcrack formation from residual gas expansion, and no discoloration from oxidative byproducts. When engineers map these degradation thresholds against cycle parameters, they can push terminal sterilization of heat-sensitive polymers further than traditional guidelines suggest, all while keeping the chain structure pristine.
Custom Sizing That Doesn't Slow Down Production
When a buyer asks for a cabinet that’s 43.2 inches wide instead of 42, most shops feel a familiar slowdown coming. That’s exactly the friction we engineered out of our process. Requests for non-standard lengths, depths, or hole patterns drop straight into the production queue without a separate round of quoting, drafting, or supplier calls.
The trick isn’t magic—it’s parametric design with hard-coded material rules. Our CAD files auto-adjust to the entered dimensions, and nesting software generates cutting paths from the same file used for the quote. Because the constraints are baked in at the template level, there’s no need for a design engineer to redraw each custom unit or double-check every edge condition.
That means a fully custom size leaves the factory on the same lead time as the closest standard option, and it doesn’t carry an upcharge for oddball numbers. You get the exact fit your space needs without watching the calendar slip.
Documented Process Control Beyond the ISO Certificate
Most organizations treat documented process control as a binder that gets dusted off before the surveillance audit. That mindset misses the point. The ISO certificate confirms a snapshot, but the real value shows up in how the documentation behaves between audits—when a machine drifts out of tolerance or a supplier sends a nonconforming batch. The procedure either guides a clear, recorded response or it gets bypassed under pressure. If the latter happens, the certificate is just wall art.
A living system goes beyond a controlled document register. It includes revision triggers that don't wait for the annual review, ownership that extends past the quality manager, and training records tied to actual task performance rather than signature sheets. Teams update work instructions when they discover a better way, not because an auditor asked. That quiet rhythm—update, verify, communicate, repeat—is what separates a certificate holder from a genuinely controlled operation.
FAQ
A reliable sheath balances stiffness at the proximal end for pushability with a soft, atraumatic tip that won't damage the vessel. The real test is how the material transitions along the shaft—abrupt changes cause kinking, so request bend radius data and simulated insertion footage, not just product photos.
Look beyond leak testing. The hub bond should tolerate repeated torque and side-port manipulation without cracking or delamination. Ask for cycle fatigue data and samples from multiple lot runs, because small molding inconsistencies often show up only after hundreds of uses.
You want a balance of column strength and flexibility—materials like lubricious Pebax or nylon blends can work, but the grade and durometer profile are what prevent kinking in tight curves. Request hardness maps along the shaft and kink-resistance benchmarks under body temperature, not just room temperature specs.
A hydrophilic coating may look good on paper, but its durability matters more than its initial lubricity. Ask about coating adhesion after repeated passes through a hemostasis valve and after sterilization, because flaking or uneven wetting can increase friction and particle risk.
Request post-sterilization dimensional data and mechanical property retention after multiple autoclave or EtO cycles, depending on your terminal method. Many polymers shift slightly and can compromise the hub fit or tip shape, so sample batches should be tested after the exact sterilization load configuration you plan to use.
Ask for capability studies on ID and OD across multiple shifts and material lots, not just a certificate of conformance. A narrow variation in wall thickness directly affects catheter compatibility and hemostasis, so look for in-process laser measurement or vision inspection systems rather than end-of-line sampling alone.
Tapered tips and side holes can introduce stress risers if the tip-forming process is not tightly controlled. A manufacturer should be able to explain how they radius transitions and validate burst pressure after tip modifications, because custom shapes often weaken the distal end unexpectedly.
You should receive full material traceability, biocompatibility test summaries according to ISO 10993, and design history files that align with your own QMS. If a supplier hesitates to share validation reports or change control records, that's a red flag for long-term production stability.
Conclusion
Choosing an OEM partner for introducer sheaths means looking past marketing claims and into the details that show up during actual use. The first thing to verify is whether the chosen polymer can handle repeated insertions without cracking, softening, or losing dimensional stability. A sheath that deforms after a few passes creates friction and risks vessel trauma. Just as important is coating consistency: many suppliers can apply a hydrophilic layer to a short sample, but the real test is whether that lubricity stays uniform from hub to tip across the full working length. Inconsistent coating leads to uneven pushability and unexpected resistance in tortuous anatomy. Distal tip geometry also deserves close scrutiny. The tip must be soft enough to track over a guidewire without digging into the vessel wall, yet firm enough not to fold or "fishmouth" during advancement. Matching the tip shape to the intended guidewire diameters and clinical access route prevents insertion failures that only surface in real procedures.
Beyond physical performance, the manufacturing process itself tells you whether a supplier can sustain quality over time. Sterilization is often an afterthought, but repeated cycles—whether ethylene oxide, gamma, or e-beam—can embrittle certain polymers or degrade coatings. Ask for data showing mechanical properties after the exact sterilization method and number of cycles your product will face. Custom sizing is another area where speed and precision must coexist. A manufacturer that quotes long lead times for non-standard French sizes or lengths may lack flexible tooling or efficient changeover processes. Finally, look for documented process control that goes deeper than an ISO certificate hanging on a wall. Suppliers should be able to show in-process inspection data, lot traceability, and deviation handling for the specific introducer sheath line you are evaluating. Without that level of transparency, even a well-designed sheath can drift out of spec once production scales.
Contact Us
Contact Person: Jeffrey
Email: [email protected]
Tel/WhatsApp: 86-0633-2230056
Website: https://www.sd-intmedical.com