OEM Assembly Cylinder Head: Key Considerations for Engine Rebuilds
2026-11-02
Engine rebuilds live or die by decisions made long before assembly. A quality OEM assembly cylinder head isn’t a luxury—it’s the baseline for compression, cooling, and valve control that budget parts can’t guarantee. Yet even experienced builders overlook a few critical details. Here’s what to watch, and why DDR deserves a look before you commit.
Why a Straight Edge Isn't Enough for Identifying a Warped Deck
A straight edge rests against the deck and shows you gaps along a single line, but warping rarely follows that kind of neat geometry. Cards can cup across their width, twist from corner to corner, or develop a subtle saddle shape that a ruler laid across the middle will simply miss. If you only check one axis, you are confirming flatness in one direction while ignoring the two others.
Even on the axis you do test, pressure from your hand or the ruler itself can flatten a mild warp just long enough to fool the eye. Card stock also reacts to humidity and temperature changes after you lift the straight edge, so a deck that looks acceptable in a dry room may bow again within minutes. That is why a straight edge gives a snapshot, not a diagnosis.
A better check combines sighting down the edges from multiple angles, gently flexing the deck in both hands, and comparing how it sits on a flat surface without any tool pressing it down. The straight edge can be a starting point, but treating it as the final word will let plenty of warped decks slip through.
The Forgotten Role of Core Shift in Cylinder Head Cooling
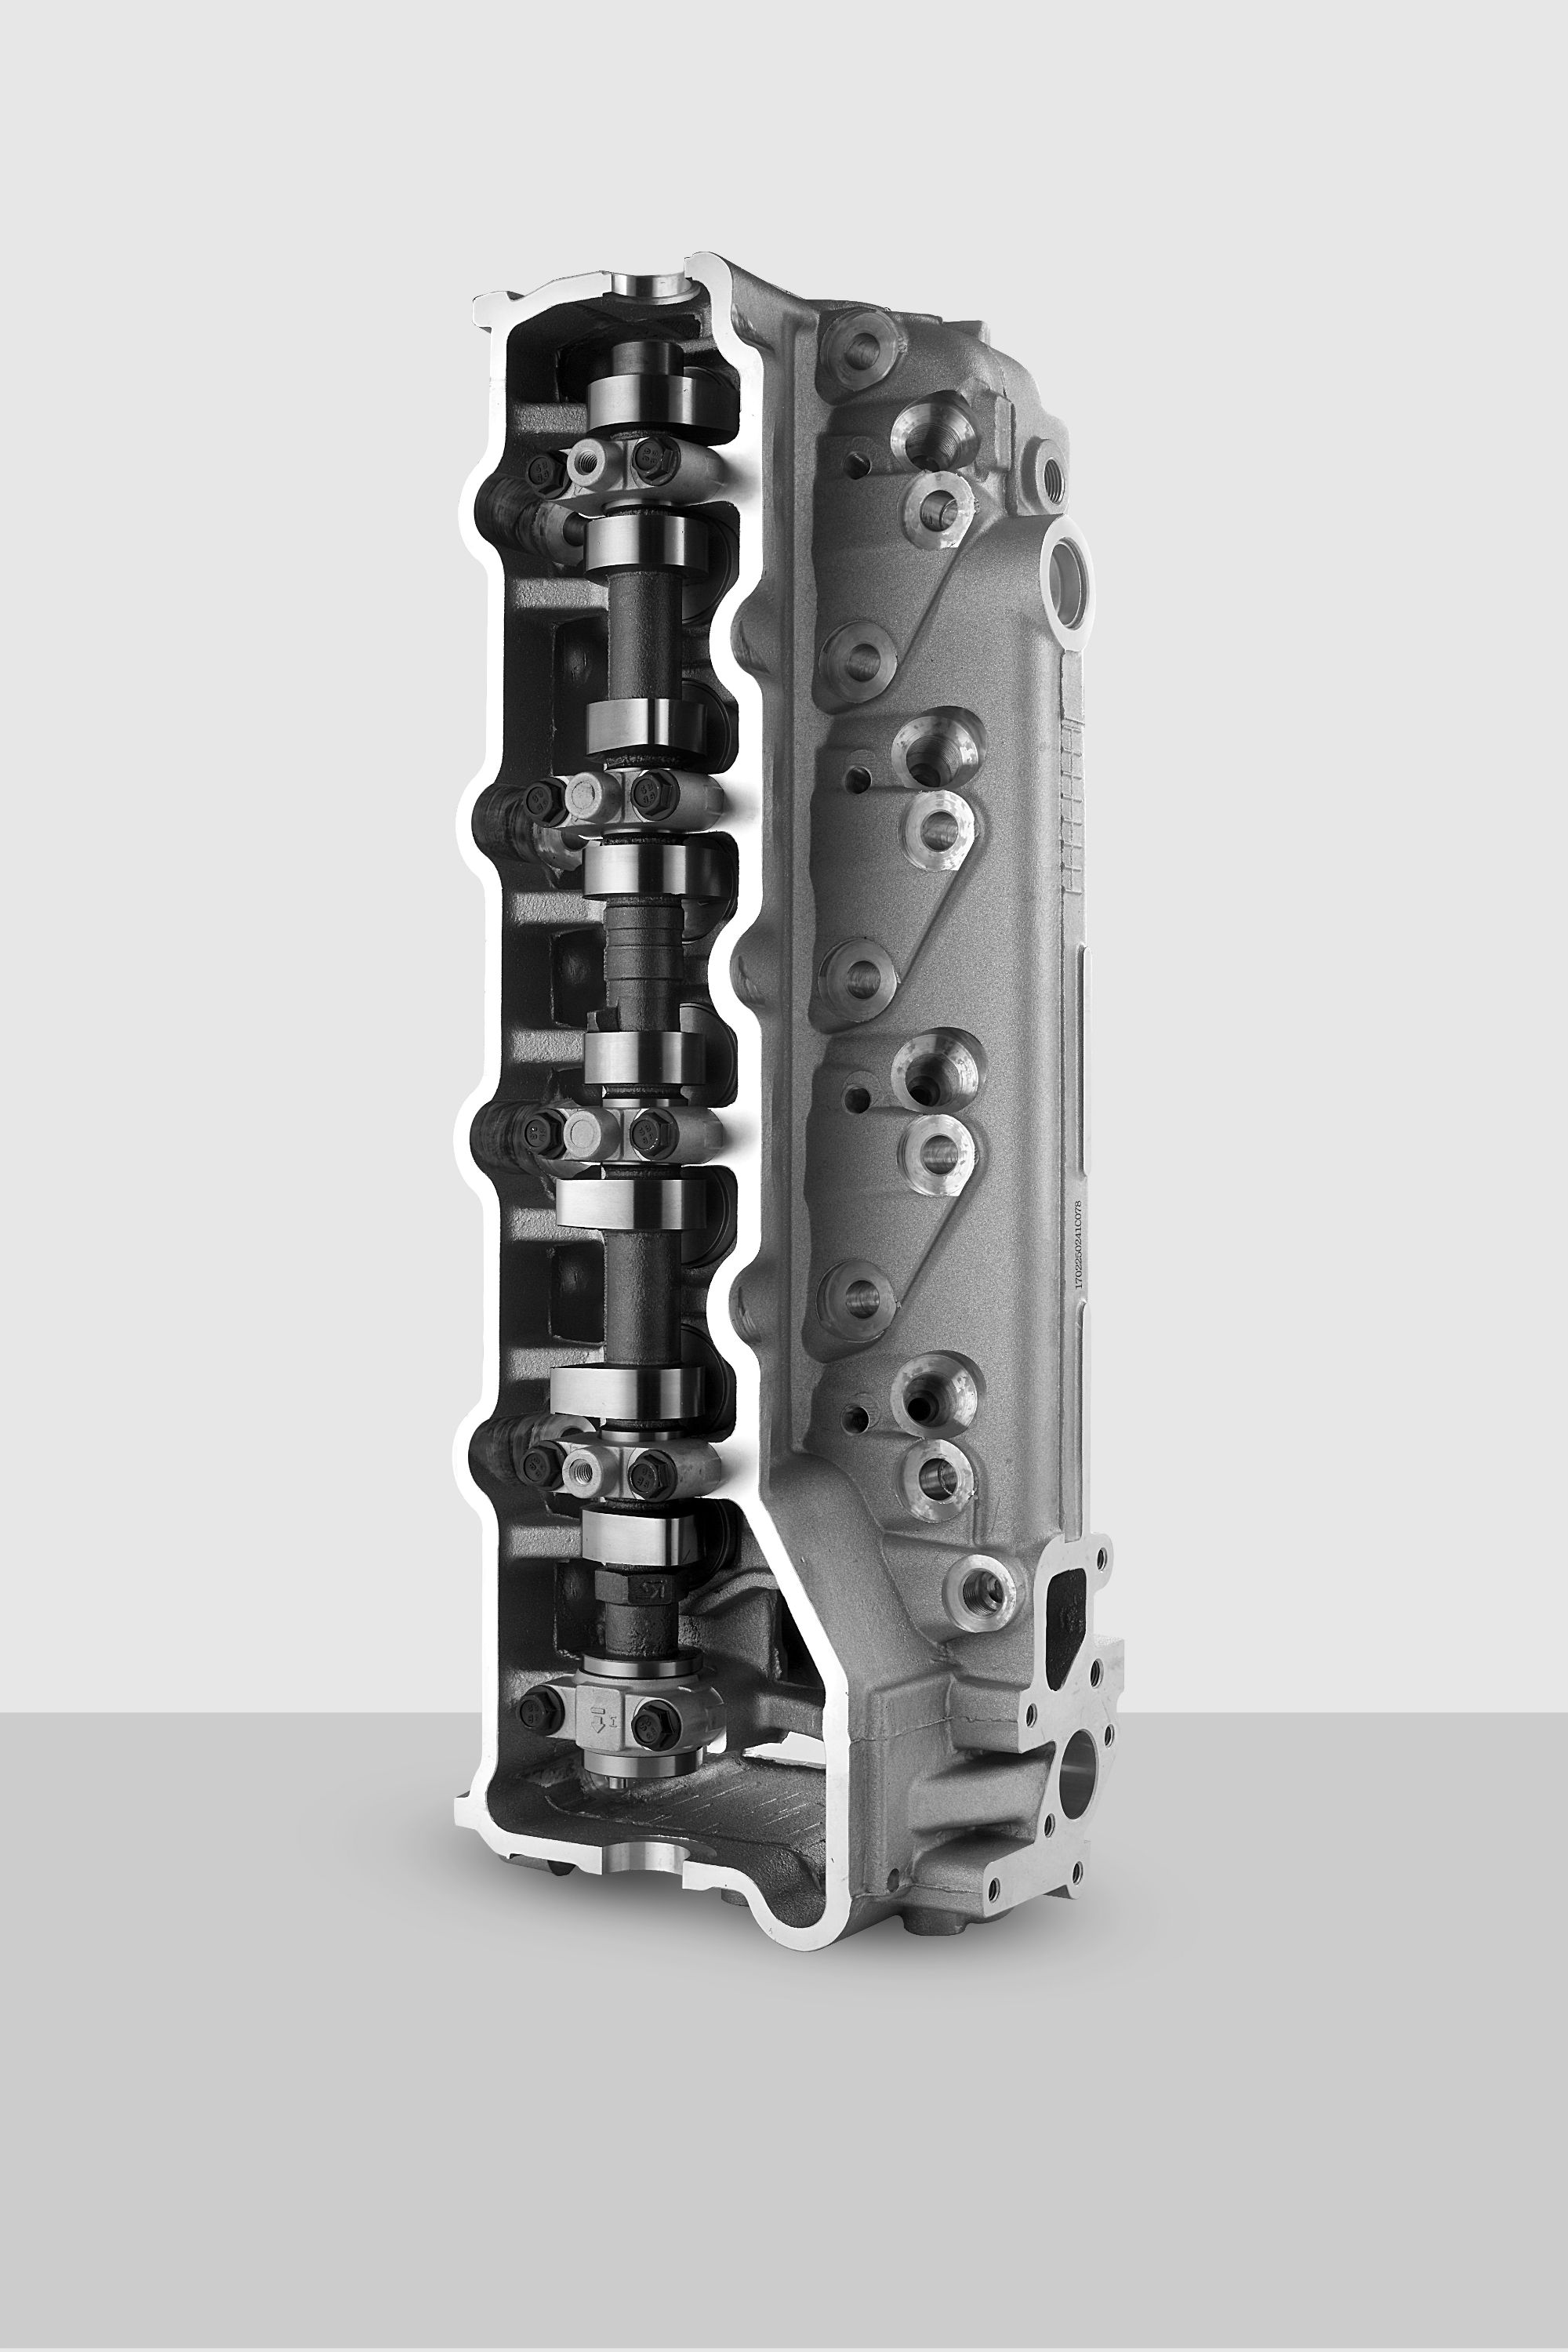
Core shift is a quiet manufacturing flaw that rarely gets blamed for overheating. When the sand cores that form water jackets and internal passages are placed in the mold, they can shift slightly as molten metal is poured. A movement of just one or two millimeters changes the wall thickness between the combustion chamber and the coolant passage. One side of the jacket narrows while the opposite side opens up. The thin side restricts coolant flow, encourages steam pockets, and creates localized boiling that can crack valve seats or warp the deck surface.
Most cooling system analysis assumes the casting matches the blueprint. Real cylinder heads rarely do. This explains why two identical engines can behave differently: one runs at normal temperature while the other develops hot spots under load. Foundries seldom measure core shift after casting because they focus on external dimensions and leak tests. A head can pass a pressure test yet still have a jacket section narrow enough to cause detonation or exhaust valve distortion. Repair shops often write this off as a bad casting, but the pattern is more systematic than most people realize.
Valve Spring Pressure and Its Direct Link to Rebuild Longevity
Many rebuilds fail early not because of machining errors or parts quality, but because the valve springs were either reused without testing or replaced with the wrong pressure. Spring pressure is what keeps the valve following the cam lobe instead of bouncing off the seat or floating at high rpm. Once that control is lost, you get valve-to-piston contact, uneven seat wear, and a sharp drop in compression long before the rest of the engine is ready to retire.
The direct link to longevity shows up in two ways. Too little pressure lets the valve bounce on the seat, which hammers the valve face and seat ring, accelerates keeper and retainer wear, and can lead to dropped valves. Too much pressure, on the other hand, puts constant load on the cam lobes, lifters, and pushrods. That extra friction and wear shortens the life of those parts and often mushrooms valve tips. A proper rebuild weighs spring pressure against the actual cam profile, max rpm, and intended use.
It is not about buying the stiffest spring on the shelf. Matching open and closed pressures to the cam card keeps the valvetrain stable without beating itself apart. That balance is what separates a rebuild that lasts 100,000 miles from one that comes back with a miss, a wiped lobe, or a sunken valve after a few thousand.
When Aftermarket Valves Create More Problems Than They Solve
Swapping in a set of aftermarket valves often feels like a straightforward upgrade until the engine starts misbehaving in ways that didn't exist before. A valve that's slightly too long can kiss the piston at high RPM, bending the stem just enough to cause a subtle misfire that no scan tool will flag. Meanwhile, a valve made from a different alloy may expand at a different rate than the guide, leading to intermittent sticking when the head gets hot—a problem that disappears by the time you pull the valve cover to inspect.
Flow bench numbers look impressive on paper, but they rarely tell you about the headaches of guide wear accelerated by a poor surface finish or a keeper groove cut a few thousandths off location. Spring pockets that need machining, tip heights that throw off rocker geometry, and seat pressures that demand a different cam profile—these are the hidden costs that get discovered only after the first track day or long tow. The stock valves may have been boring, but they were coordinated with the rest of the system.
There's also the matter of quality variance between batches. One set drops in without a hitch and runs for years; the next from the same brand shows inconsistent stem diameters or a valve face that never quite seals. By the time you've done a leak-down test, pulled the head, and lapped or replaced the offending valves, the money saved over OEM parts has vanished into gaskets, coolant, and another weekend in the garage.
Bolt Hole Prep and the Illusion of Proper Clamping Force
Torque wrenches create a comforting sense of precision, but the number on the dial is mostly a measure of friction, not stretch. A bolt hole that hasn't been cleaned leaves rust, old thread locker, or cutting oil in the thread path. Those contaminants eat up a large share of the applied torque before any useful clamp load develops, so the wrench clicks at spec while the joint remains loose. This is the core illusion: you think you've hit proper clamping force, but you've only hit a friction target.
Prep work changes what the torque reading actually means. Running a thread chaser through the hole, scrubbing the bolt threads, and checking the under-head surface for burrs all reduce variability. Lubrication matters even more. A lightly oiled thread and a dry, gritty thread can produce wildly different preload at the same torque. If the hole is blind, leftover debris at the bottom can hydro-lock or bottom out the fastener, giving a false tight feel. None of this shows up on a standard torque wrench.
The real goal is repeatable clamp load, not a magic torque number. Without consistent hole prep, even a calibrated wrench is just guessing. Some joints benefit from torque-angle monitoring or direct stretch measurement, but those only work if the threads and mating surfaces start in a known state. Clean holes, controlled lubrication, and flat washers under the bolt head are not optional details; they are what separate a properly clamped joint from one that merely feels tight.
What a Pressure Test Misses About Hairline Combustion Chamber Cracks
A standard pressure test pushes coolant or compressed air through the water jacket to reveal leaks, but hairline combustion chamber cracks often stay hidden because they only open under extreme thermal expansion. At room temperature the metal contracts, sealing the fracture tight enough to hold pressure. The test can pass with flying colors while the crack waits for operating heat to yawn wide.
These micro-fissures usually form between valve seats or near the spark plug threads, where casting walls are thin and temperature swings are brutal. Unlike a blown head gasket that shows constant seepage, a hairline crack behaves like a one-way valve, bleeding combustion gas into the cooling system only at full load. Static pressure testing never replicates that dynamic flexing, so the crack remains invisible until you pull the head and inspect with dye penetrant or a fine borescope under magnification.
The real giveaway is often indirect: coolant disappearing without external drips, sporadic overheating at highway speeds, or combustion byproducts in the radiator. Chasing those symptoms with repeated pressure tests wastes time. A good machinist will heat the head in an oven before pressurizing, or use a vacuum test on a warm engine, because cold static checks miss exactly the failure mode that matters most.
FAQ
OEM assemblies come straight from the manufacturer with new valves, springs, seals, and guides already fitted and tested together. You skip the variables of a shop's machining quality and get components that were designed to work as a set, which reduces the chance of uneven wear or premature failure after the rebuild.
No. Most modern engines use torque-to-yield bolts that stretch permanently once tightened. Reusing them can lead to uneven clamping force and head gasket leaks. Always check the service manual, but plan to replace head bolts or studs unless they're explicitly listed as reusable.
Even new parts deserve a quick once-over. Look for any shipping damage on the gasket surface, confirm all oil and coolant passages are free of debris or protective coatings, and verify that the cam bearing surfaces feel smooth. A clean lint-free wipe with brake cleaner on the deck surface also removes any residual preservative.
It's not just about hitting the final number. The sequence and incremental steps matter because they spread clamping force evenly across the head and block. Skipping the middle torque stages or tightening in a random order can warp the head or crush the gasket unevenly, leading to compression leaks.
You can, but it's often a false economy. The old rockers, lifters, or cam followers have worn into the previous head's geometry. Mixing them with a fresh head may create noise, accelerated wear, or improper valve lift. If the budget allows, swap in the matching new valvetrain components that the OEM assembly was designed around.
Flushing the block's coolant passages before installing the new head. Old scale, rust, and silicate gel can hide in the block and then circulate into the new head's narrow passages, causing hot spots and warpage later. A thorough block flush and fresh coolant are cheap insurance.
For a daily driver or work vehicle that needs to stay reliable, usually yes. You're paying for factory-matched components, known valve clearances, and no hidden cracks or previous overheating damage. A used or reman head might save money now, but a failure means doing the job twice and paying for another head gasket kit.
Rushing the first start and ignoring break-in. Prime the oil system, turn the engine over without fuel or spark until you see oil pressure, then follow the cam and ring break-in procedure if applicable. The first 20 minutes matter more than the next 20,000 miles for seating parts and preventing scuffing.
Conclusion
When rebuilding an engine, the cylinder head often gets less scrutiny than it deserves. A straight edge and feeler gauge might catch an obvious bow, but they won't reveal a deck that's warped in multiple planes or has localized high spots around head bolt bosses. That uneven clamping leads to gasket failure down the road. Core shift—the slight misalignment of internal sand cores during casting—is another hidden variable. It can leave water jackets thinner on one side, so a head that cools fine on the bench may run hot in the car. Valve spring pressure is equally easy to overlook; used springs lose tension unevenly, and without checking each one at installed height, you're gambling with valve float and seat bounce long before the next rebuild.
Aftermarket valves often look tempting, but oversize stems or mismatched seat angles can ruin an otherwise careful valve job. The same goes for bolt hole prep: if threads aren't chased and lubricated consistently, your torque wrench reads a number that doesn't match actual clamping force. Finally, a standard pressure test only checks for gross water jacket leaks. Hairline cracks in the combustion chamber, especially around valve seats, stay hidden until the engine is hot and under load—by then the head is already scrap. A thorough rebuild means checking more than the obvious specs.
Contact Us
Contact Person: Shelly
Email: [email protected]
Tel/WhatsApp: 8613967667688
Website: https://www.yongyu.com/