Industrial Furnace Spare Parts Factory Essentials for Reliable High Temperature Operations
2026-09-07
When the heat is on, literally, your furnace is only as strong as its weakest spare part. But how do you separate parts that survive from parts that thrive? In this post, we explore the fundamentals every industrial furnace spare parts factory must master for reliable high-temperature operations. And if you're serious about uptime, you'll want to see how THINKING-LONG approaches the challenge differently.
Alloy Fixtures and Baskets: Designing for Thermal Fatigue, Not Just Load
Most fixture designs start with a simple question: can it hold the part without yielding? That’s fine for room-temperature tooling, but in heat-treat operations the real killer is rarely a single overload. It’s the slow accumulation of micro-cracks from repeated expansion and contraction. A basket that looks overbuilt on paper can fail in weeks if the designer treated thermal stress as an afterthought. The alloys we use—cast nickel-chromium grades, for instance—don’t just carry weight; they breathe with every cycle. Ignore that, and you’ll see distortion, sagging, and eventual fracture in places no load calculation would predict.
Thermal fatigue in fixtures shows up in predictable patterns: cracks initiating at sharp corners, weld toes, or section changes where stress concentrates. The fix isn’t always thicker material, though that’s the lazy response. Often it’s about geometry—generous radii, tapered transitions, and avoiding abrupt mass differences. A heavy solid bar next to a thin expanded-metal panel will expand at different rates, forcing the weaker member to strain beyond its limit. We’ve replaced solid crossbars with ribbed or split designs that flex slightly, letting the whole basket move as one unit instead of fighting itself.
Material selection matters more than most shops admit. A low-cost stainless like 304 will oxidize and embrittle under repeated quenching, while a higher-nickel alloy like RA330 or 600 holds its ductility longer. But even the best alloy fails early if the design ignores thermal gradients. Quench fixtures, for example, see the outer edges cool faster than the core. That gradient creates internal tension every single cycle. Slots, holes, and cutouts should be oriented to let heat escape evenly, not trap it. And don’t weld everything rigid—sometimes a bolted or pinned joint with a little clearance is the difference between a fixture that lasts three months and one that runs three years.
The Case for Stocking Extra Insulation Modules, Not Just Bricks
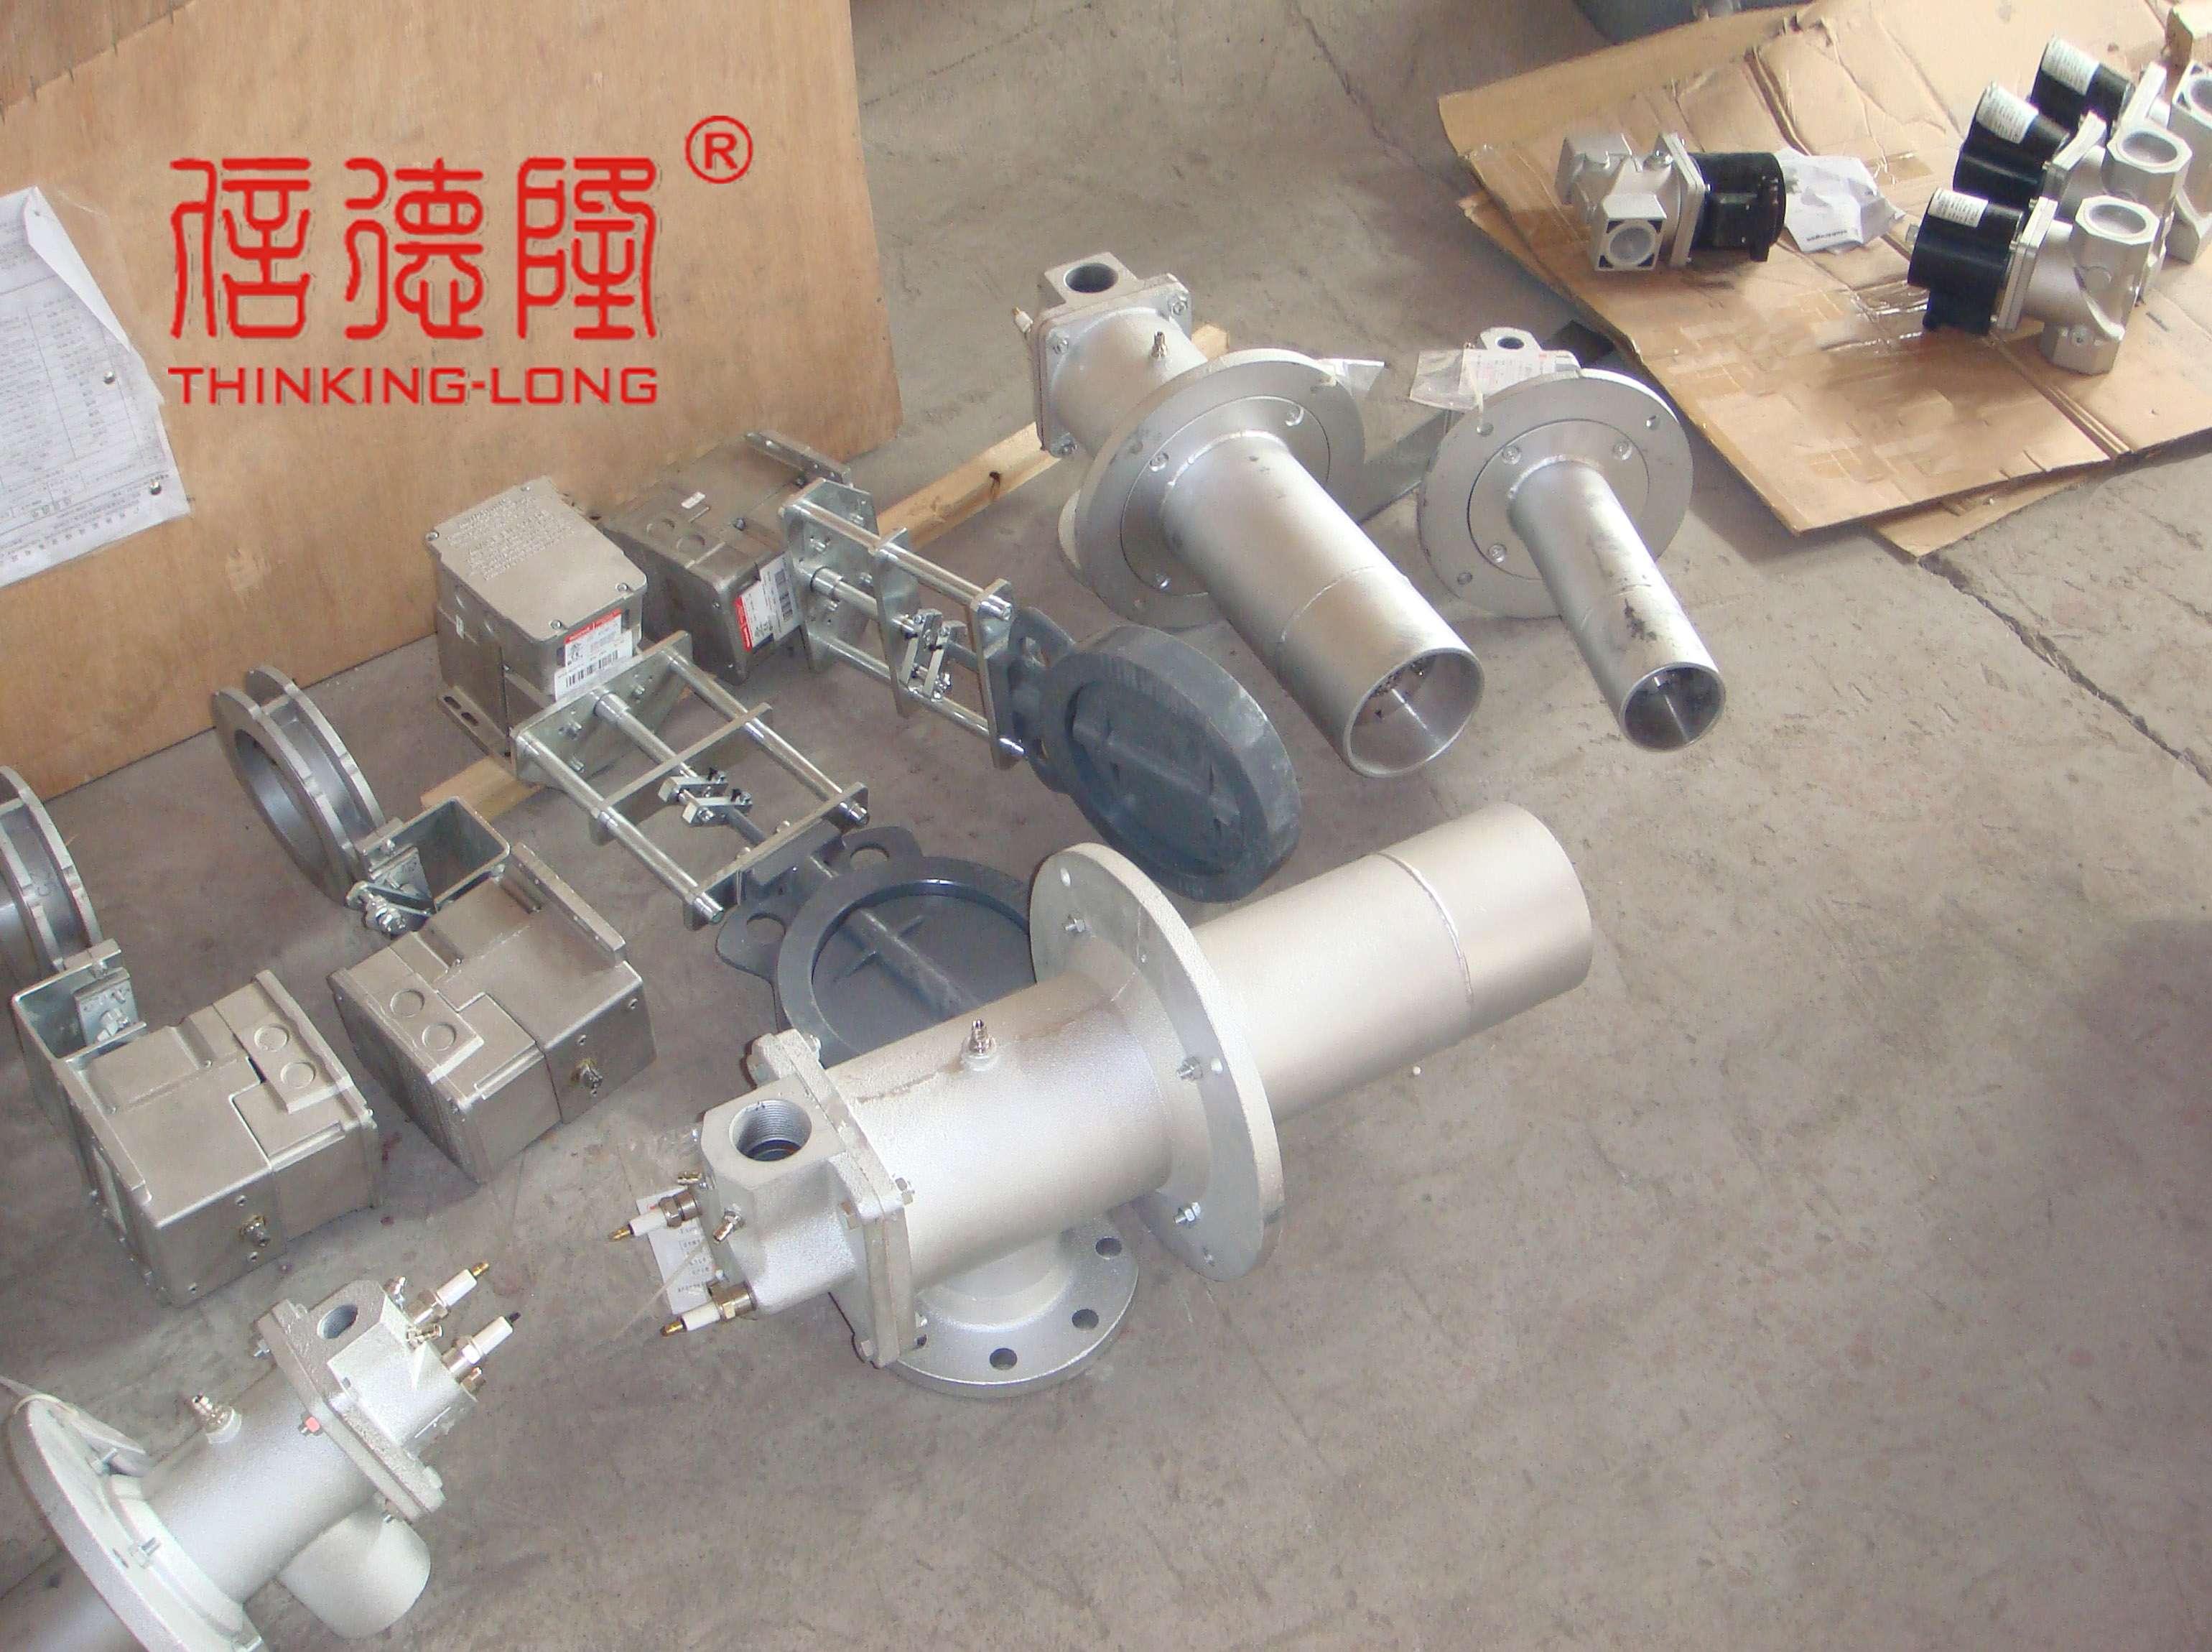
Stocking extra insulation modules alongside bricks changes how quickly a project can adapt to thermal performance requirements. Bricks offer mass and durability, but they do little on their own to slow heat transfer. Insulation modules arrive pre-sized to fit wall cavities, roof gaps, and awkward transitions, so crews can install them without cutting rigid foam on site. Having a surplus means a single change in building codes or client preferences does not stall the schedule.
Insulation modules also reduce long-term operating costs in ways that extra bricks cannot. A wall with integrated modular insulation maintains indoor temperatures with less energy input, which matters more as utility rates fluctuate. Because the modules stack flat and weigh less per unit volume than brick, storage takes up less floor space, and transport to upper floors becomes easier. In many retrofit jobs, the ability to slip a module behind existing cladding avoids the need to rebuild brick sections entirely.
Finally, stocking only bricks assumes every future repair will be structural. Many callbacks involve condensation, drafts, or uneven temperatures—problems solved by adding insulation, not masonry. Keeping extra modules on hand turns those fixes into a same-day task rather than a special order. It is a practical hedge against the most common site delays, and it usually costs less than carrying excess brick that may sit unused for months.
Quick Checks for Silicon Carbide Rods Before Each Campaign
Before firing starts, run your fingers along the cold rod surface—glaze cracks or hairline fractures often hide under dust. A quick resistance check with a multimeter beats waiting for a mid-campaign failure; drift beyond 10% from baseline usually signals aging or localized damage.
Next, check the terminal clamps and contact straps. Loose connections cause arcing and uneven heating, which can shorten rod life dramatically. Give each clamp a slight wiggle—if it shifts, tighten it to the manufacturer’s torque rather than just snugging it down.
Finally, look for white or brown spots near the hot zone. Those are early signs of oxidation or silica bloom, and they tend to spread once the kiln reaches temperature. Mark the spots with a soft pencil so you can compare after the campaign and decide if rotation or replacement is due.
Why Your Furnace Door Seal Fails Faster Than the Lining
Furnace door seals live a much harder life than the lining. Every time the door swings open or clamps shut, the seal gets compressed, sheared, and scraped against the door frame. The lining just sits there, exposed to heat but not to that kind of mechanical abuse. Over hundreds of cycles, the seal's fibers or braided structure start to break down long before the refractory bricks show any real wear.
Heat cycling adds another layer of punishment. The seal expands and contracts with each temperature swing, and because it's thin and flexible, it can't absorb those stresses the way a thick lining can. At high temperatures, organic binders in the seal burn out, leaving it brittle and prone to cracking. Meanwhile, the lining might develop hairline cracks too, but they rarely propagate fast enough to cause failure within the same timeframe.
Chemical attack hits the seal from both sides. Flue gases, slag vapors, and even ambient moisture work their way into the seal's porous structure, accelerating corrosion. The lining usually has a denser, more chemically resistant hot face, so it holds up better. But the seal is the weak link at the edge of the door, where turbulence and leakage are worst. That's why seal replacement often becomes a routine job while the lining soldiers on for years.
A No-Nonsense Spares Budget for Peaks Above 1,300°C
At 1,300°C and above, spare parts don't fail on a predictable schedule. Thermal shock, oxidation, and creep work together to shorten the life of heating elements, thermocouples, and insulation. Build your spares budget from actual cycle data, not from a generic list. Track hours at temperature for each hot-zone component, then set a reorder point at roughly 70% of the worst-case lifespan you have seen over twelve months.
A practical spares kit for these temperatures should include at least one set of silicon carbide or molybdenum disilicide heating elements, two or three spare type R or type S thermocouples, a roll of high-alumina fiber blanket, and enough castable refractory to patch small cracks. Budget for one complete hot-zone rebuild per furnace every two to three years, depending on how often you push above 1,350°C. That line item alone often costs more than all other spare parts combined, so plan for it separately.
Don't overlook the less glamorous line items: expedited freight for a failed element on a Friday night, spare alumina tubes for protection sheaths, and a few extra terminal clamps or straps. A no-nonsense budget includes 10 to 15 percent on top of parts pricing for urgent shipping and unplanned downtime. Review actual consumption every quarter and adjust quantities only when you see a pattern of early failures, not after every single surprise.
Lead Times You Should Actually Plan Around for Custom Castables
Standard refractory products often ship within a few days because they sit on a shelf, already mixed and boxed. A custom castable is a different animal entirely. Once you approve the formulation, the clock starts on raw material checks, precise weighing, and batch mixing that cannot be rushed without risking performance. The lead time you see on a general product page rarely reflects what happens when your blend includes non-stock aggregates or a binder that has to be ordered in.
In practice, you should plan for at least two to four weeks between order confirmation and dispatch for most custom castables. If your mix requires a trial batch or physical property testing before full production, add another week or more. Suppliers will sometimes quote shorter windows assuming everything goes perfectly, but equipment scheduling, lab availability, and incoming raw materials often slide. Ask for the number of calendar days to shipping, not just “typical” turnaround, and confirm whether the timeline starts at order entry or after all technical details are locked.
Build your installation schedule around a realistic delivery date, not the day you hope the material arrives. Factor in freight time, site access, and a buffer for re-testing if a batch fails an internal check. The most common mistake is treating custom castables like an off-the-shelf item and discovering too late that the material won’t be on site when the crew is ready. A short conversation with the manufacturer about actual production capacity and current backlog will save more time than any expedited shipping option.
FAQ
A part intended for sustained furnace duty must combine the right alloy composition with a microstructure that resists creep and oxidation. For instance, nickel-chromium grades with small additions of rare earth elements form a tenacious oxide scale that slows further attack. Beyond chemistry, the casting or forging process must avoid internal voids that expand unevenly at heat. Finally, dimensional tolerances should anticipate thermal growth so the component doesn't distort or bind against adjacent parts.
Instead of stocking every possible component, focus on the few items whose failure stops the whole line: radiant tubes, burner tips, hearth rollers, and thermocouple protection sheaths. Tag each with expected lead time and a minimum reorder threshold based on real usage, not a generic formula. Keep critical parts in a dry, vibration-free area because moisture absorbed in ceramic fiber or refractory anchors can cause steam spalling when heated. A shared spreadsheet or simple kanban board works better than complex software if it's updated by the maintenance crew after every event.
Fasteners and support hardware rarely get the same attention as heating elements, yet a failed bolt can bring down a whole insulation module. Inconel 601 or 330 stainless are common choices, but even better is using the same alloy family as the adjacent components to avoid galvanic or differential expansion issues. Ceramic fiber anchors need a molybdenum or alumina coating if they will be exposed to direct flame impingement. Also consider the purity of alumina in electrical insulators; cheap grades with high silica content can become conductive at temperature, causing short circuits and false temperature readings.
Two parts with the same chemical analysis can behave differently because of grain structure and trace impurities. A casting with coarse, columnar grains may crack along grain boundaries after repeated thermal cycles, while a fine-grained forging withstands the same conditions. Hidden contaminants like sulfur or lead, even in parts-per-million concentrations, can drastically reduce hot ductility. Surface finish matters too: deep machining marks act as stress risers where cracks initiate. Therefore, a supplier's process control and post-casting heat treatment often matter more than the nominal alloy specification.
Every material expands at a different rate, and a rigid connection between two unlike metals will shear or buckle as the furnace heats up. For example, a stainless steel radiant tube welded to a carbon steel flange will develop high stress at the weld interface. Proper design allows for sliding joints, expansion loops, or flexible couplings. Even within a single component, uneven heating creates internal stress: a thick wall section next to a thin one can crack if the temperature gradient exceeds about 50°C per centimeter. So spare part drawings should include clear notes on allowable clearance and preload to accommodate thermal movement.
Rapid temperature swings are far more damaging than steady-state heat because they cause fatigue from cyclic expansion and contraction. One useful practice is to mark critical parts with temperature-indicating paints or irreversible labels that show the maximum surface temperature actually reached. Keep a log of every quench or emergency cool-down event and compare that history against the part's rated cycle life. When installing replacement parts, run a low-temperature bake-out cycle to drive off moisture and volatiles before the furnace returns to full service. Also perform a hot alignment check on moving parts like rollers or doors after the first 24 hours of operation.
Most coatings fail by spalling, which is driven by the mismatch in thermal expansion between coating and base metal. A simple test is to heat a small sample to service temperature, quench it in air, and repeat a few dozen times while watching for hairline cracks or flaking. If the part will be exposed to combustion gases, also check for carburization or sulfidation, which can turn a protective oxide layer into a brittle scale. Ask the supplier for accelerated cycling test data or perform your own by placing coated coupons in the actual exhaust stream for a week. The results often surprise people: a cheap aluminide coating may outperform an expensive ceramic overlay in a specific gas atmosphere.
Look for surface changes that signal internal damage: bulging, sagging, or a change in color from gray to black or green often indicates oxide scale buildup or alloy depletion. On radiant tubes, measure the outside diameter at several points; a reduction of more than 2-3% usually means wall thinning from oxidation or erosion. Listen for new rattling or vibration during operation, which can mean that internal supports have cracked. Regular thermographic imaging can spot hot spots where insulation has degraded or where a part is overheating due to misalignment. Finally, keep track of electrical resistance in heating elements; a gradual increase beyond 10-15% of the initial value means the element is consuming itself and should be replaced before it opens the circuit.
Conclusion
Reliable operation above 1,300°C starts with spare parts that are chosen for how they fail, not just what they carry. Alloy fixtures and baskets may look sturdy under a static load, but repeated thermal cycling is what actually opens cracks at welds and corner joints. Opt for designs with generous radii and expansion allowance rather than just heavier sections. Insulation is another case where conventional stocking logic falls short: the modules around burner blocks and roof penetrations break down far sooner than the dense brickwork, so keeping spare modules on hand prevents a small hot spot from turning into a forced shutdown. Silicon carbide rods deserve a five-minute inspection before every campaign—look for uneven surface oxidation, hairline cracks near the cold ends, and any drift in resistance readings. Catching those early avoids a mid-cycle failure that can damage adjacent refractories.
Furnace door seals are a classic weak point because they endure both mechanical abuse and thermal shock every time the door opens. The lining might last for years, but the seal can harden, crack, or lose compression within months, so treat it as a consumable with a much shorter replacement interval. When setting a spares budget for extreme temperatures, allocate more than the usual percentage to items that degrade through creep and oxidation—radiant tubes, retorts, hangers, and castable anchors. Custom castables add another layer of planning: their lead times are dictated by raw material availability and curing schedules, not by your maintenance calendar. Place orders before the previous lining campaign ends, and keep a written record of actual delivery times so future shutdowns stop being hostage to supplier backlogs.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/