Hollow Wall Winding Pipe Machine Factory Manufacturing Process Explained
2026-11-16
Most people only ever see the finished hollow wall winding pipe—smooth, sturdy, ready for burial. Few get to walk the factory floor where raw polymer is transformed into that spiral-wound structure under heat, pressure, and precise control. At COMRISE, that process isn't a mystery; it's a carefully choreographed sequence we're about to break down step by step. If you've ever wondered how a machine can continuously wind a hollow wall with consistent wall thickness and weld strength, this behind-the-scenes look will answer it—and might change how you spec your next project.
Prepping Raw Material for the Winding Machine
Before a coil takes shape, the raw material has to earn its spot on the payoff. I usually run a clean fingertip along the edge and look for burrs, flat spots, or dull patches that don't show up on the spec sheet. If the stock came from a cold warehouse or sat next to a bay door, I'll let it rest near the machine until it stops fighting the tensioner. That small wait beats wrestling a half-set spool through the first hundred feet.
Setting up the payoff gets more attention than people think. Instead of just dropping a spool on the arbor, I'll adjust the drag until the rotation feels lazy and even, then mark the flange with a grease pencil so the next shift can repeat the same feel. A quick wipe with a lint-free cloth removes supplier dust or leftover oil before the first foot feeds into the guides. That extra minute up front usually saves me from clearing a tangle mid-run.
The Spiral Winding Sequence That Creates the Hollow Core
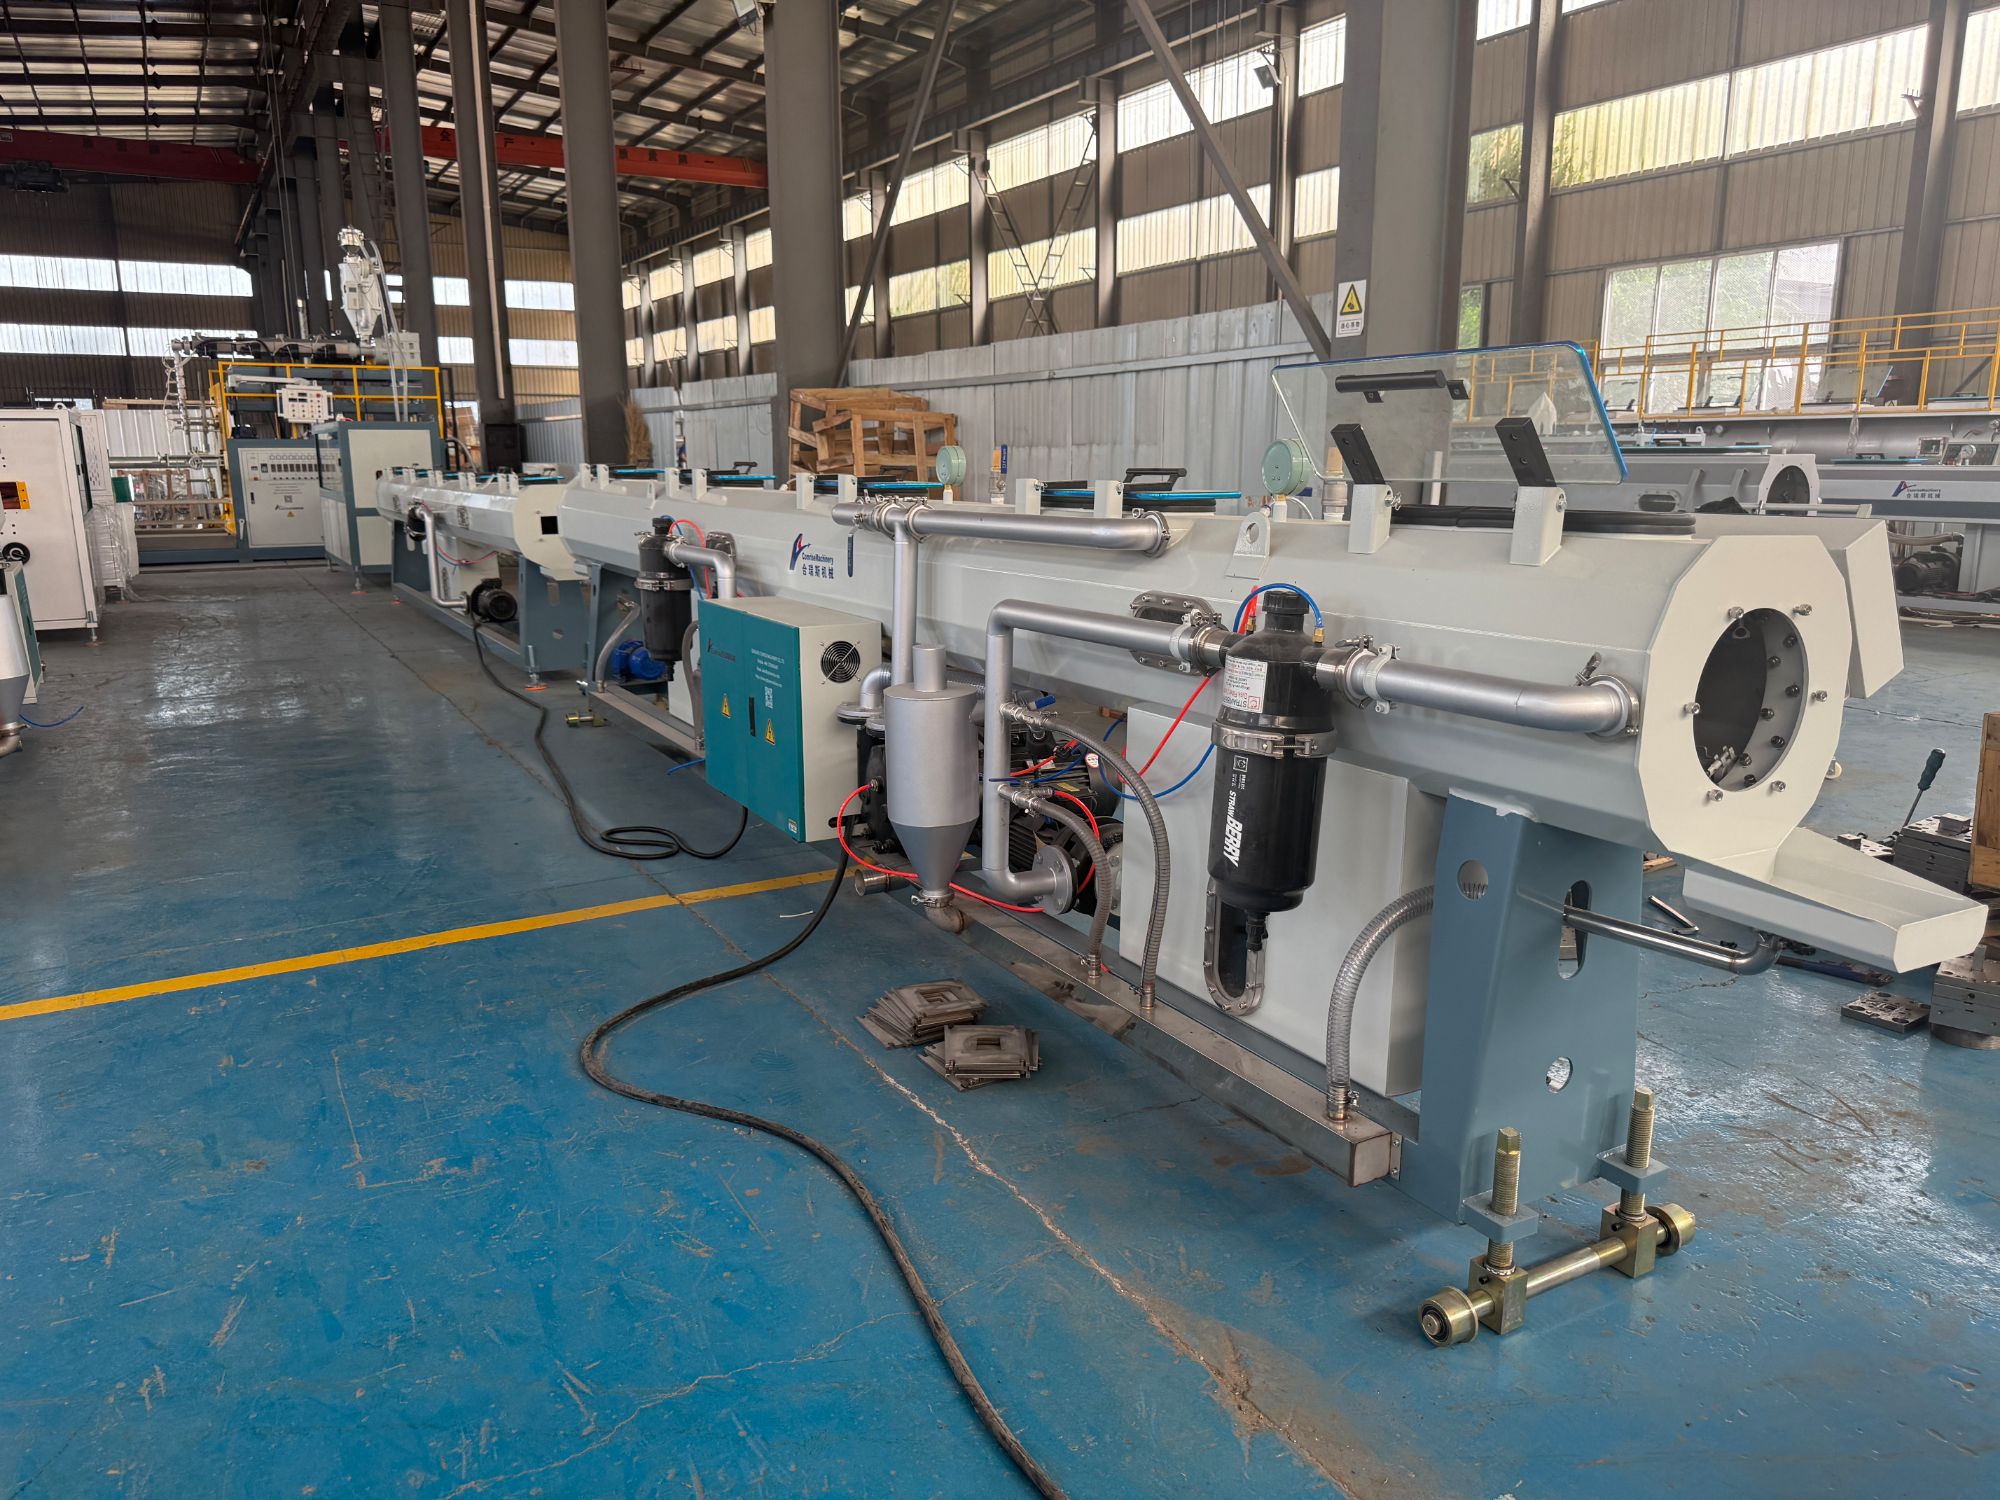
At the heart of the process is a tensioned filament or tape that approaches a rotating mandrel at a carefully calculated angle. Instead of laying down in simple rings, each pass advances slightly along the mandrel’s axis, so the material crosses over itself in a continuous helix. The angle, usually kept between 20 and 70 degrees depending on the required hoop-to-axial strength ratio, decides how much the core will resist crushing versus bending. As successive layers build up, the overlapping pattern locks the fibers into a self-supporting lattice, eliminating the need for internal supports beyond the removable form.
The real precision comes in reversing the feed direction at the ends of the mandrel. A single winding pass would leave gaps, but by reversing the carriage before the material reaches the edge, the next layer crosses at the opposite angle, forming a diamond-shaped mesh. This back-and-forth sequence repeats until the wall thickness reaches its design value, typically with each layer adding only a fraction of a millimeter. Because the crossing points are evenly distributed, there are no weak seams—just a continuous, interwoven tube that holds its shape once the mandrel is extracted.
What makes the hollow core possible is that the winding does not rely on adhesive to fill voids; the tension itself keeps every fiber in elastic contact with the layer beneath it. After the final pass, the assembly is cured or hardened, then the mandrel is pulled out along the axis, leaving behind a smooth interior surface that mirrors the mandrel’s finish. The result is a structure with no glued joints, no internal ribs, and a perfectly uninterrupted cavity ready for fluid flow, wiring, or reinforcing fill.
Heat Bonding Turns Wound Layers Into a Solid Pipe Wall
During filament winding of thermoplastic composite pipe, each tape or tow is deposited under tension while the contact zone is heated beyond the resin's melting point. The heat softens the surface of the incoming layer and the previously wound substrate, allowing polymer chains to interdiffuse across the interface. Upon cooling, the separate layers solidify into a continuous matrix with no discrete boundaries, effectively erasing the layered structure.
The quality of this transformation depends on controlling heat input, consolidation pressure, and winding speed. Too little heat leaves weak interfaces that can delaminate under load, while excessive heat causes resin degradation or fiber displacement. Common heating methods include hot gas, infrared, or laser, each aimed at creating a narrow molten zone that fuses the layers without disturbing fiber alignment.
Once properly bonded, the wall behaves as a single homogeneous shell rather than a stack of loosely adhered plies. This eliminates micro-voids and stress concentrations between layers, improving hoop strength, leak tightness, and resistance to cyclic pressure. The result is a solid pipe wall that can handle demanding service conditions while maintaining tight dimensional tolerances.
Cooling and Diameter Calibration on the Production Line
In most profile or pipe extrusion setups, the cooling stage does more than just harden the melt. A well-designed vacuum tank pulls the hot surface against a calibrator sleeve, locking in the outer dimensions before the material has a chance to sag or swell. Water temperature and flow are adjusted zone by zone, because an overly aggressive quench can create a frozen skin while the core is still molten, leading to voids or warpage later.
Diameter calibration is rarely a set-and-forget task. Non-contact gauges, often laser or ultrasonic, continuously read the part's cross-section and feed that data back to the haul-off and extruder speed controls. If the line runs a bit fast, the product gets pulled thin; too slow and it bulges. Skilled operators tend to make small, gradual corrections instead of chasing every minor fluctuation, which keeps the process stable.
In practice, the best results come from treating cooling and calibration as one linked system. Changing the water level in a vacuum tank can shift the diameter just as much as adjusting screw speed, and a worn calibrator sleeve will gradually open up tolerances no matter how precise the gauges are. That's why line audits usually focus on both the mechanical condition of the calibration tooling and the actual temperature profile along the cooling path.
Cut-to-Length and Quality Gates Every Pipe Must Pass
Every pipe that leaves the line starts with a length call that’s tighter than most people expect. Cut-to-length isn’t a rough step; the saw is set against a calibrated stop and checked with a laser at the start of each shift, and any drift past a millimeter pulls the batch for reset. Operators don’t eyeball it—they tag the first cut, measure it at three points, and only then let the rest of the order run.
After cutting, each pipe moves through a series of quality gates that feel less like checkboxes and more like physical stops. At the first gate, a burr check and bevel inspection catch edge damage before it can hide under a bundle wrap. The second gate runs a wall-thickness probe and compares the result to the heat number on file. If the numbers don’t line up, the pipe is taken off the rollers right there.
The last gate is about accountability, not just compliance. A pipe only gets its final stamp after the cut length, end condition, and material trace have all been signed off by someone on the shift. If there’s a gap in that trail, the pipe sits in a quarantine rack until someone can explain it. That’s what keeps mismatched lengths and questionable ends from ever reaching the delivery truck.
Final Handling from Factory Floor to Shipping
Once a unit rolls off the line, it enters a short but tightly monitored buffer zone before it ever sees a truck. Here, final functional checks are repeated under real-world load conditions, not just pass/fail diagnostics. Minor cosmetic issues get corrected at the workstation rather than held for a separate rework queue, which keeps the flow steady and avoids last-minute surprises at the dock.
Packing is matched to the actual route and destination rather than a one-size-fits-all standard. Orders heading to humid climates get extra vapor barrier film, while those moving through rough freight lanes use reinforced corner blocks and strapping points already mapped on the pallet. Labels are printed only after the last inspection sign-off, so the serial, customer part number, and carrier barcode all line up with what is physically on the pallet.
From the staging lane, the load moves directly into a pre-assigned outbound bay. The shipping clerk verifies seal numbers and weight slips against the bill of lading before the driver is cleared to depart. Any variance triggers a side-by-side recount before the dock door closes, because correcting an error at the factory costs minutes, while fixing it after dispatch costs days.
FAQ
The main frame is typically fabricated from Q235 or Q345 structural steel plates that are cut, bent, and welded into box sections. After welding, the frame goes through vibratory stress relief so it stays dimensionally stable during high-speed winding operations.
Each roller shaft is mounted in adjustable bearing housings. Technicians use a laser alignment tool to check runout across the full length, then shim the housings until the total indicated runout is under 0.1 mm. This prevents uneven pipe wall thickness later.
For rotating components, gas metal arc welding with a mixed shielding gas is preferred. After welding, the cage is dynamically balanced on a balancing machine to reduce vibration at the operating speed, which is usually between 20 and 80 rpm depending on pipe diameter.
The screw is checked for straightness using a dial indicator on a lathe bed. The flight OD is measured at several points to ensure uniform clearance with the barrel. Any deviation over 0.05 mm per meter means the screw is sent back for re-machining or polishing.
Not a full production run, but the machine goes through a dry run where all drives, heaters, and cooling fans are cycled. Then a short calibration run is done with recycled polyethylene or polypropylene to verify that temperature zones hold within plus or minus 3 degrees Celsius and the winding speed matches the setpoint.
The hollow wall reduces weight while maintaining ring stiffness. The machine creates the hollow profile by wrapping a profiled strip or multiple strips around a rotating mandrel, with the rib cavities formed by the shape of the winding rollers and the overlap width of each pass.
They should check the chain tension on the main drive, look for plastic buildup around the trimming knives, verify that the heating bands on the extruder are clamped tight, and listen for any irregular noise from the support rollers. Catching a loose bearing early is much cheaper than replacing a shaft later.
Typically the base machine is designed for straight pipes with a constant diameter. Some factories add a separate winding station or adjustable forming shoes for sockets and spigots, but full manhole production usually requires a dedicated machine because the wall geometry and winding angles are quite different.
Conclusion
Inside a hollow wall winding pipe factory, the process starts with raw polymer pellets—usually HDPE or PP—being dried and fed into a single-screw extruder. The molten ribbon exits the die at a controlled temperature and width, then wraps around a slowly rotating mandrel. Rather than a simple spiral, the machine lays each pass with a slight overlap, creating a continuous hollow core that gradually builds up wall thickness. Operators watch the winding head closely; any fluctuation in melt pressure or mandrel speed shows up immediately as a visible gap or ridge in the pipe surface.
Once the wound layers reach the target wall thickness, a bank of hot-air nozzles or infrared panels fuses the overlaps into a solid, void-free wall. The still-soft pipe then passes through a vacuum calibrator and cooling spray section, where the outer diameter is locked to within a fraction of a millimetre. An inline laser gauge checks the OD continuously, and any drift beyond tolerance triggers an automatic correction. At the cut-off station, a planetary saw slices the pipe to order length. Every length is then pressure-tested and visually inspected for surface defects before it gets chamfered, stamped, and packed onto timber pallets with stretch film, ready for dispatch.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com